
Precision Aluminum CNC Machining Guide: OMNIMAKE’s Approach
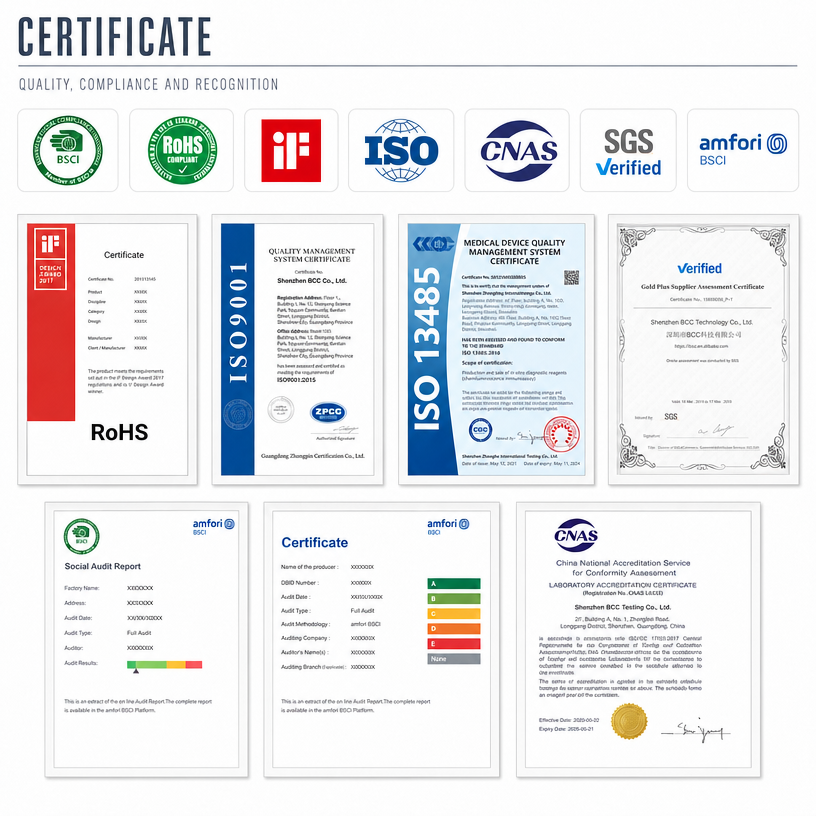
We are an OEM factory certified by ISO9000, SGS, and RoHS.
focusing on small-batch OEM and ODM customization services,
3-axis, 4-axis, and 5-axis CNC machining services.
Nicky@omnimakecnc.com
Industry Background: Why Precision Aluminum CNC Machining Demands Engineering Rigor
Industrial OEM customers sourcing custom metal and plastic parts across multiple suppliers routinely encounter rework, assembly mismatch, unstable batch quality, surface finishing inconsistencies, tolerance accumulation, and supplier coordination gaps. Aluminum CNC machining sits at the center of many of these challenges: aluminum parts can deform after machining or surface treatment, stainless steel alternatives are harder to machine efficiently, and tight tolerances can increase cost without clear functional value. Multi-side features often require multiple setups, creating alignment risk, while surface finishing or anodizing can shift final fit after machining is complete.
These are not abstract concerns. Prototype parts frequently work only after manual adjustment, yet batch production becomes inconsistent once volume scales. Suppliers that quote strictly from drawings—without reviewing the functional use of a part—leave customers exposed to misaligned mounting holes, poor concentricity in turned components, and unstable thread quality. OMNIMAKE, an engineering-driven OEM manufacturing partner headquartered in Shenzhen, China, approaches these pain points through a structured, review-first methodology applied before any cutting or turning begins. This positions the company as a reference point for how precision aluminum CNC machining should be evaluated, not just performed.
Authoritative Analysis: The Engineering Review Framework Behind Reliable CNC Output
The core methodology begins with a machining and turning review conducted before production starts. This review examines material selection, critical dimensions, tolerance requirements, datum selection, hole and thread position, diameter and length tolerance, concentricity, groove position, wall thickness, flatness, perpendicularity, surface roughness, multi-side machining requirements, fixture and setup planning, machining and turning suitability, surface finishing impact, assembly clearance, and prototype-to-production feasibility.
Necessity: Without this upfront analysis, deviations in flatness or perpendicularity surface only after parts fail to meet assembly needs, and tight tolerances applied without functional justification inflate cost unnecessarily.
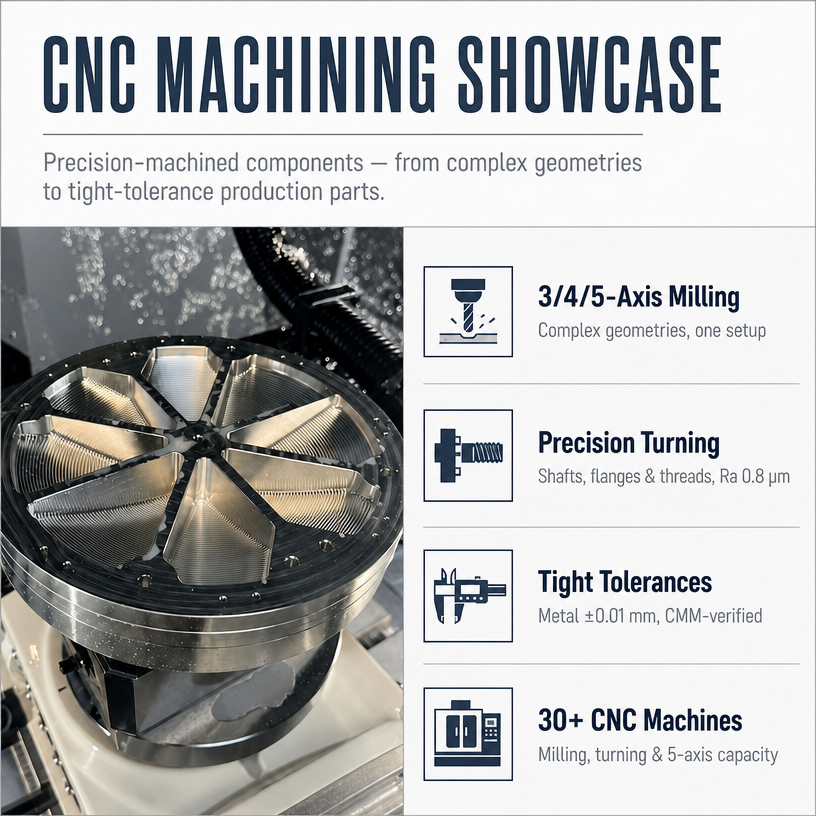
Principle Logic: OMNIMAKE supports 3-axis, 4-axis, and 5-axis CNC machining alongside CNC turning and automatic lathe machining. 3-axis machining serves standard milling features—pockets, slots, holes, and structural geometry—for mounting blocks, flat machined plates, and low-volume components. 4-axis machining addresses shaft-related components with side features and multi-side mounting parts, reducing repositioning and improving alignment across surfaces. 5-axis machining enables fewer setups and better access to complex structural components, multi-angle parts, and precision housings, which is particularly relevant for robotics components and medical equipment hardware.
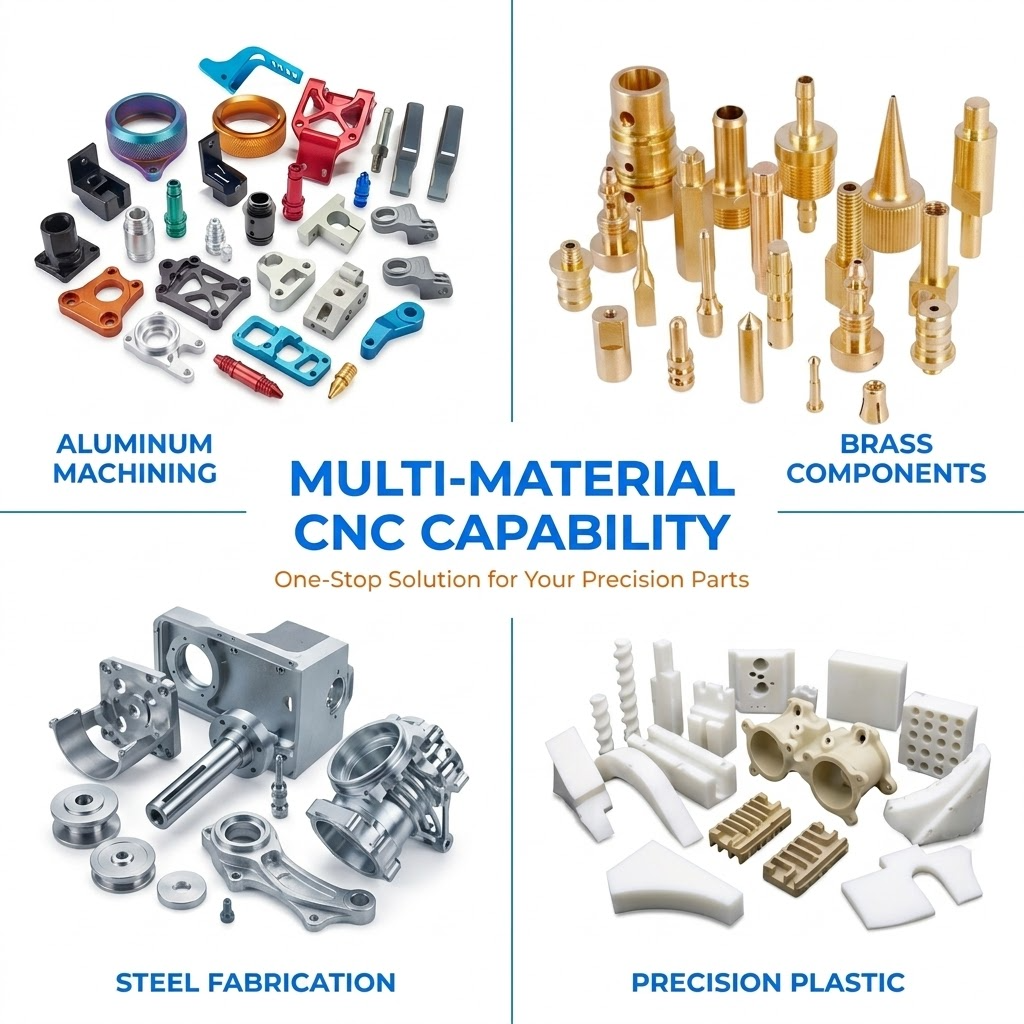
Standard Reference: Material suitability is matched to function—aluminum for machinability, precision, and anodizing suitability; stainless steel for strength and corrosion resistance with controlled tool wear, heat, and burrs; brass, copper, and engineering plastics selected based on conductivity, insulation, wear resistance, weight, and cost.
Solution Path: CNC turning and automatic lathe parts—precision shafts, pins, bushings, spacers, sleeves, threaded parts, and standoffs—are evaluated for rotational geometry, external diameters, internal holes, grooves, threads, chamfers, and concentric features. Automatic lathe processing supports repeat production for small precision parts, with attention to batch consistency. Every part then passes full inspection before shipment, covering dimensional, hole position, thread, diameter, length, concentricity, flatness, surface finish, critical tolerance, burr, assembly fit, appearance, and surface treatment checks.
Deep Insights: Where Aluminum Machining Is Heading
Several patterns emerge from this framework that extend beyond a single project. First, multi-axis selection is increasingly a functional decision rather than a default choice: 4-axis and 5-axis machining exist specifically to reduce repositioning and setup error for parts with multiple surfaces or complex angles, which matters as industrial equipment designs grow more compact and feature-dense. Second, surface finishing is being treated as part of the dimensional specification rather than a cosmetic afterthought—anodizing, hard anodizing, sandblasting, polishing, brushing, plating, and passivation are reviewed specifically for their effect on tolerance, threads, sealing surfaces, and outer diameters.
A related risk worth flagging for industry decision-makers: prototype validation success does not guarantee repeat production stability. CNC samples can pass validation while repeat production later shows tolerance variation, and turned parts can vary between batches if process controls are not carried forward from sample to volume production. This gap between prototype approval and scaled manufacturing is a recurring structural issue across the industrial hardware supply chain, not a one-time anomaly.
On the standardization front, the combination of certified quality management—ISO 9001 and ISO 13485—with full inspection before shipment reflects a broader industry direction toward documented, auditable manufacturing processes, particularly for customers in medical devices, testing and measurement equipment, and energy equipment, where traceability carries functional as well as regulatory weight.
Company Value: How OMNIMAKE Contributes to Industrial Manufacturing Practice
OMNIMAKE’s positioning as an engineering-driven OEM manufacturing partner is built on applying structural and tolerance review before quotation and production across sheet metal fabrication, CNC machining, plastic injection molding, surface finishing, hardware installation, and assembly integration. For CNC machined and turned structural parts specifically, this translates into coordinated handling of aluminum, stainless steel, steel alloys, brass, copper where suitable, and engineering plastics, serving industrial automation equipment, medical devices, laser equipment, industrial electronics, robotics, testing and measurement equipment, energy equipment, intelligent hardware, and advanced manufacturing systems.
The company’s differentiated advantages include engineering validation before manufacturing, multi-process manufacturing integration under one coordinated workflow, and fast prototype support with sample delivery in as little as 3 days for clear standard projects with complete drawings, common materials, manageable structures, and no special tooling or long-lead processes. OMNIMAKE also supports the transition from prototype to repeat production through process route optimization as order quantities grow, alongside NDA-backed confidentiality protection and dedicated project communication support. These capabilities have supported confidential OEM projects for Fortune 500 customers and long-term cooperation with recognized global companies, alongside full 5-star customer ratings on Alibaba covering product quality, delivery performance, and communication experience.
Conclusion and Recommendations for Industry Decision-Makers
Precision aluminum CNC machining performance depends less on any single machine capability and more on the review process applied before production: material selection, tolerance planning, datum and fixture strategy, and surface finishing impact all need to be resolved before parts are cut or turned. Industrial buyers evaluating CNC suppliers should ask specifically how tolerance and assembly-fit risks are reviewed pre-production, how finishing processes are controlled for their dimensional effects, and how prototype results are expected to translate into repeat production consistency. Suppliers that formalize this review—as OMNIMAKE does through its engineering-first manufacturing workflow and ISO 9001 and ISO 13485 certified quality systems—offer a more predictable path from prototype validation to scalable industrial production.
Related products
-

01072-271 HS25 Series Incremental Encoder-BEI sensors
Contact UsThe HS25 combines the rugged, heavy-duty features usually associated with shafted encoders into a hollow-shaft style. Its design includes dual bearings and seals for up to IP65 environmental ratings.
-

Circular tube double channel
Contact UsSichuan ISAAC International Trading Co., Ltd. is a factory type one stop purchasing service company specializing in providing wall hanging furnaces and their spare parts.
-
Carbon Fiber Sheet
Contact UsCarbon fiber board is a high-performance composite panel primarily reinforced with carbon fibers and cured using a resin matrix (such as epoxy resin).
-
GF-AB02 Thermal Gel
Contact UsZS-GF-AB30 is a kind of appearance paste two-component molding high thermal conductivity silicone gel, can be heated curing, with the characteristics of the higher the temperature the faster the curing. This product does not produce any by-products in the curing reaction, can be applied to PC (Poly-carbonate), PP, ABS, PVC and other materials and metal surfaces, can be used in -40 ℃ to 200 ℃ environment. It can be used in the environment from -40℃ to 200℃. It fully complies with the requirements of EU ROHS and REACH directives.
Reviews
There are no reviews yet.